
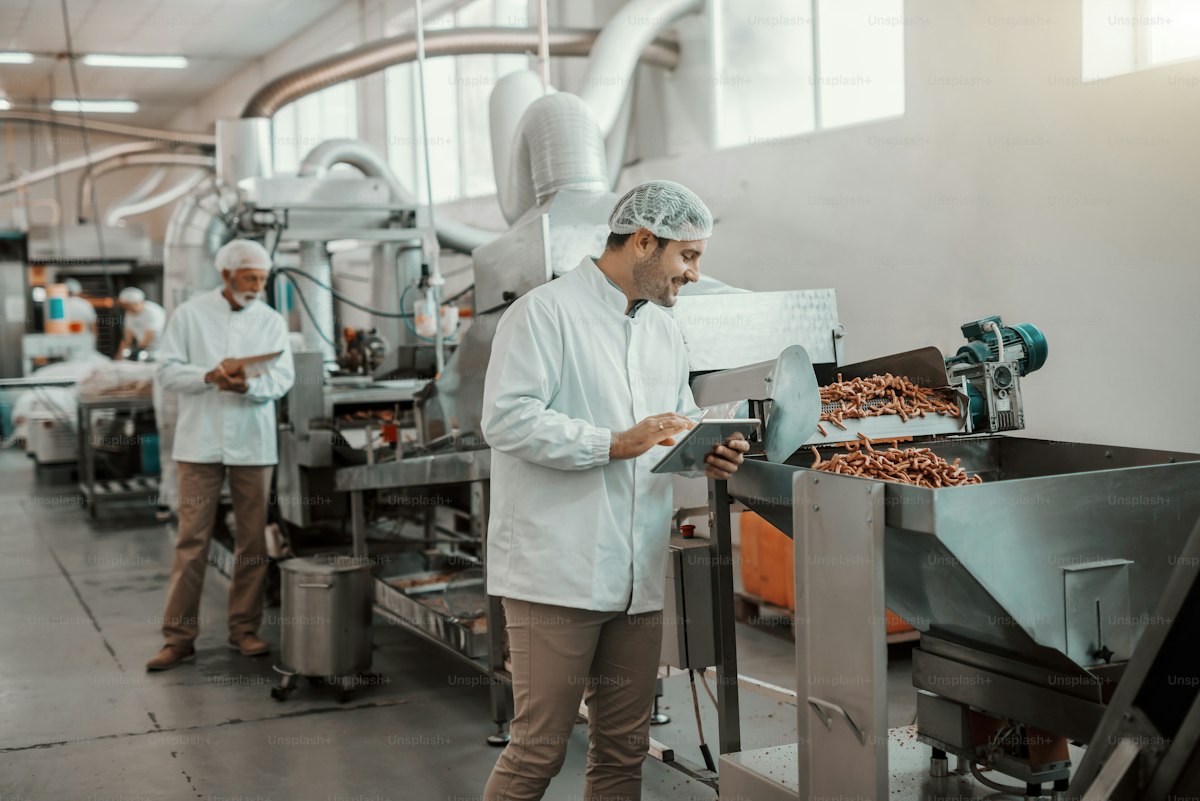
The primary paradigm shift within food processing engineering entails moving away from retrospective end-product microbiological testing toward proactive, preventative systems. Established by NASA, the Natick Laboratories, and the Pillsbury Company in the 1960s to ensure zero microbiological defect in spaceflight rations, the Hazard Analysis and Critical Control Points (HACCP) methodology provides a structured kinetic framework to eliminate, prevent, or reduce food safety hazards to acceptable thresholds across linear processing lines.
1. Introduction: Prerequisite Frameworks and Hazard Analysis Principles
A valid HACCP architecture relies upon verified prerequisite programs: Good Manufacturing Practices (GMP) and Standard Sanitation Operating Procedures (SSOP). During preliminary hazard evaluation, every unit operation (intake, thermal dwell, chilling, metal detection, aseptic packaging) is assessed across biological (a_w, pH, spore germination), chemical (mycotoxins, unlisted allergens, sanitizing residues), and physical vectors (ferrous metal fragments, brittle glass splinters) using quantitative Risk Priority Matrices (Probability × Severity).
2. Technical Analysis: Decision Trees, Critical Limits, and Processing Case Studies
Not every point of vulnerability qualifies as a Critical Control Point (CCP). Applying the Codex Alimentarius Logic Tree establishes whether a preventative control step exists downstream. If the designated operation represents the ultimate stage capable of eliminating the target hazard, it is designated as a mandatory CCP.
Fluid Milk Pasteurization Engineering Case Study: In continuous plate heat exchanger (PHE) milk pasteurization, the thermal holding tube constitutes CCP-1. The critical thermodynamic limit is defined as ge 72°C held for a minimum hydrodynamic dwell of 15 seconds. This thermal lethality protocol targets complete vegetative inactivation of resilient zoonotic pathogens (Coxiella burnetii and Mycobacterium bovis). If temperature falls to 71.9°C, automated pneumatic Flow Diversion Valves (FDV) instantly actuate within 150 milliseconds, shunting sub-pasteurized volume back to raw balance tanks without contaminating packaging silos.
| Unit Operation | Identified Hazard Class | HACCP Status | Critical Limit Boundary | Monitoring & Verification Protocol |
|---|---|---|---|---|
| Raw Grain Intake | Chemical: Aflatoxin B1 & Ochratoxin A | oPRP (Prerequisite) | Aflatoxin B1 < 2 ppb, Moisture < 13.5% | Per-lot HPLC/ELISA analysis, calibrated moisture meters |
| Fluid Milk Pasteurization | Biological: C. burnetii, Listeria | CCP (CCP-1) | Temp ge 72°C, Dwell ge 15 s | Dual PT100 sensors, thermographic logging, automated FDV |
| Inline Metal Detection | Physical: Stainless steel swarf, iron flakes | CCP (CCP-2) | Fe: le 1.0 mm, Non-Fe: le 1.5 mm | Hourly certified test wand verification, pneumatic kick reject |
| Retort Thermal Canning | Biological: Clostridium botulinum endospores | CCP (CCP-3) | F₀ ge 3.0 min (121.1°C equivalent) | Internal container thermocouple dataloggers, calibrated gauges |
3. Conclusion: Engineering Takeaways, Verification Rigor, and System Governance
HACCP operates not as static paper documentation, but as an empirical dynamic calibration system. In food manufacturing quality systems, operational monitoring must never be conflated with verification: Reading an inline temperature display every 15 minutes constitutes real-time “monitoring,” while monthly calibration against an accredited traceable mercury-in-glass reference thermometer constitutes “verification.” Zero microbiological failure is achievable solely when precision automation interfaces with uncompromising food engineering design.